Providing state-of-the-art engineering solutions, custom equipment manufacturing, and turnkey projects for the global Edible Oil & Process Industries.
Founded in 2000, Sanjay Sharma Consultancy and its sister concern, Charu Techno Projects, operate under the unified leadership and vision of Mr. Sanjay Sharma. Over the past two decades, we have established ourselves as trusted names in providing comprehensive engineering solutions across India and abroad.
We specialize in the end-to-end design, manufacturing, and commissioning of high-quality, energy-efficient, and technologically advanced process plants. From refinery sections and solvent extraction systems to heavy engineering utility structures, our execution is backed by precision engineering and sustainable value creation.

Founder & Director
Lead Mechanical & Process EngineerTailored plant capacities ranging from 5 TPD to 5000 TPD, designed in-house to suit specific workspace requirements and feedstock characteristics.
Integrating heat recovery loops, multi-stage economizers, and highly optimized thermal fluid networks to minimize operating fuel and electricity costs.
Fabrication using premium grade raw materials (SS304, SS316, and high-tensile Mild Steel) in compliance with international process safety norms.
Complete in-house engineering, from flow-sheet design and vessel fabrication to on-site mechanical erection and commissioning.
Deep expertise in modern degumming, physical/chemical oil refining, dewaxing, and high-vacuum deodorizing systems.
Smart PLC control panels, real-time temperature tracking, and safety interlocks that reduce human errors and enhance safety.
Advanced chemical engineering setups for Transesterification, Methanol recovery, and food-grade Lecithin drying units.
Comprehensive after-sales troubleshooting, spare parts supply, structural maintenance, and process efficiency audits.
Strict commitment to delivery timelines, optimized logistics management, and fast mechanical assembly on client sites.
Designed to remove phospholipids (gums), mucilage, and trace metals from crude oil. Degumming improves the efficiency of subsequent bleaching and deodorizing stages to yield a highly stable final oil.
Crude oil is heated to 60-80°C depending on oil type to reduce viscosity and ensure proper conditioning.
Phosphoric or citric acid is injected to complex trace metals and convert non-hydratable gums into hydratable forms.
A high-speed centrifugal separator discharges clear degummed oil (light phase) and hydrated gums (heavy phase).
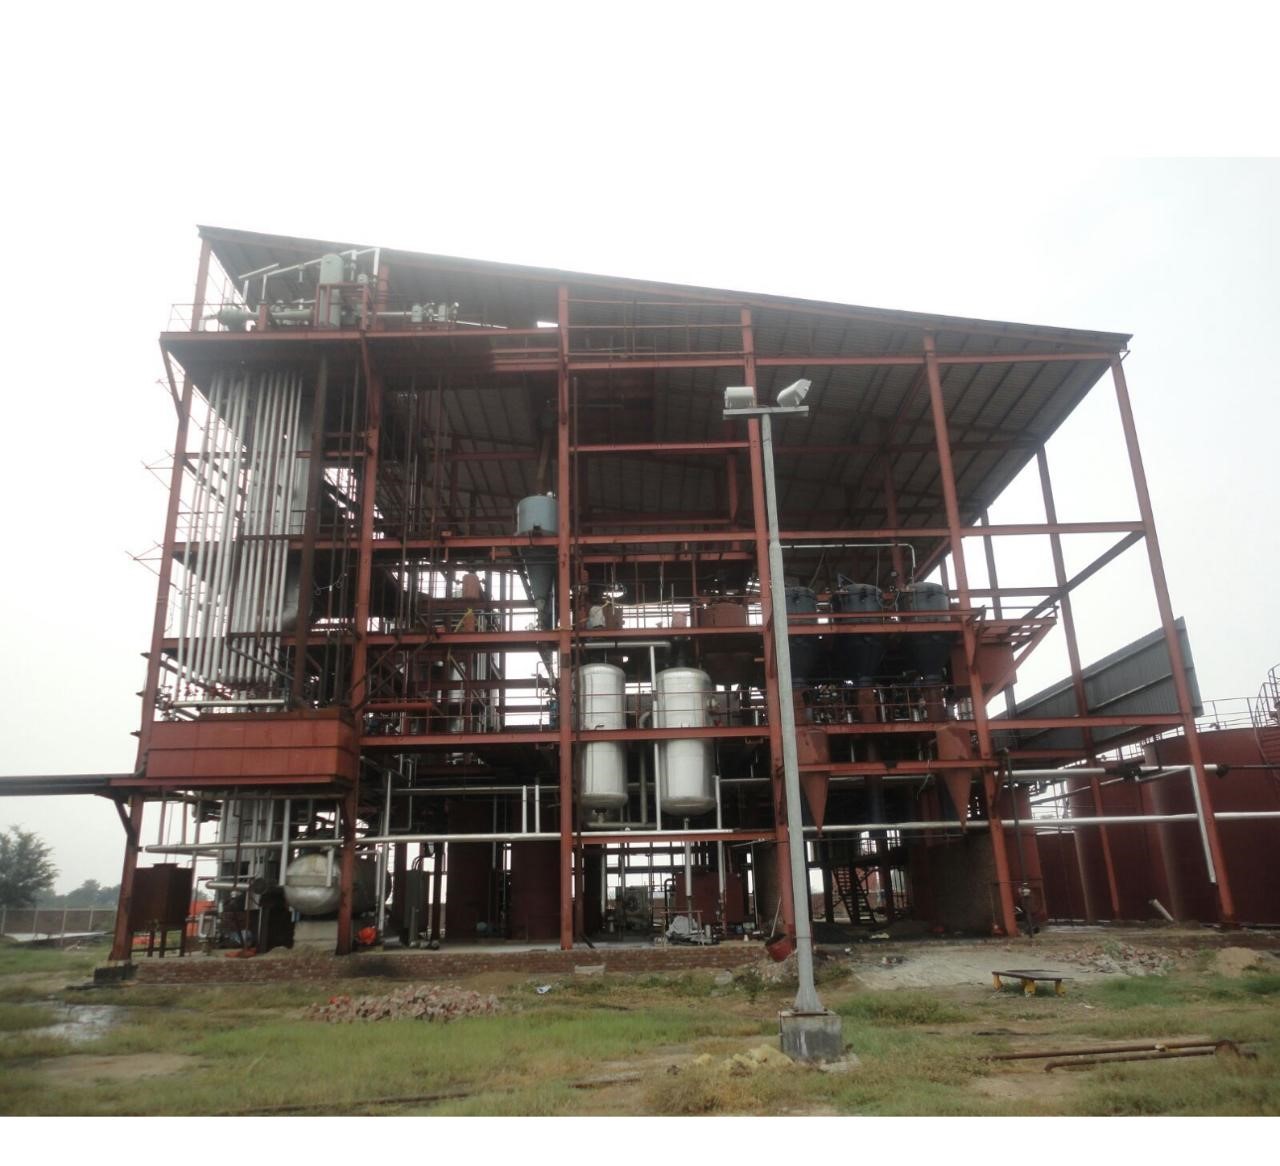 ★ Flagship Product
Our Edible Oil Refinery Plant is engineered to refine crude vegetable oils into high-quality, clear, odorless, and stable edible oils suitable for direct consumption and commercial use. Designed for efficiency, precision, and long-term reliability, the refinery system ensures superior oil quality with enhanced shelf life and improved flavor.
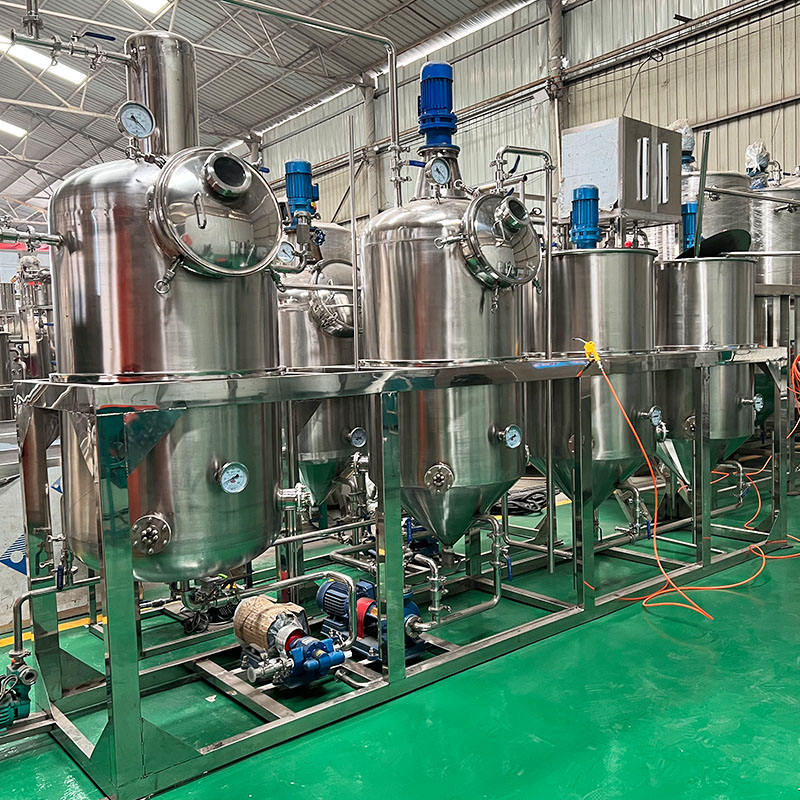 Refinery
A critical component in the refining process, the Neutralizer removes acidic impurities and free fatty acids (FFA) from crude oils using a controlled caustic soda (NaOH) mixing reaction, featuring custom vertical agitators for thorough blending and soap stock separation.
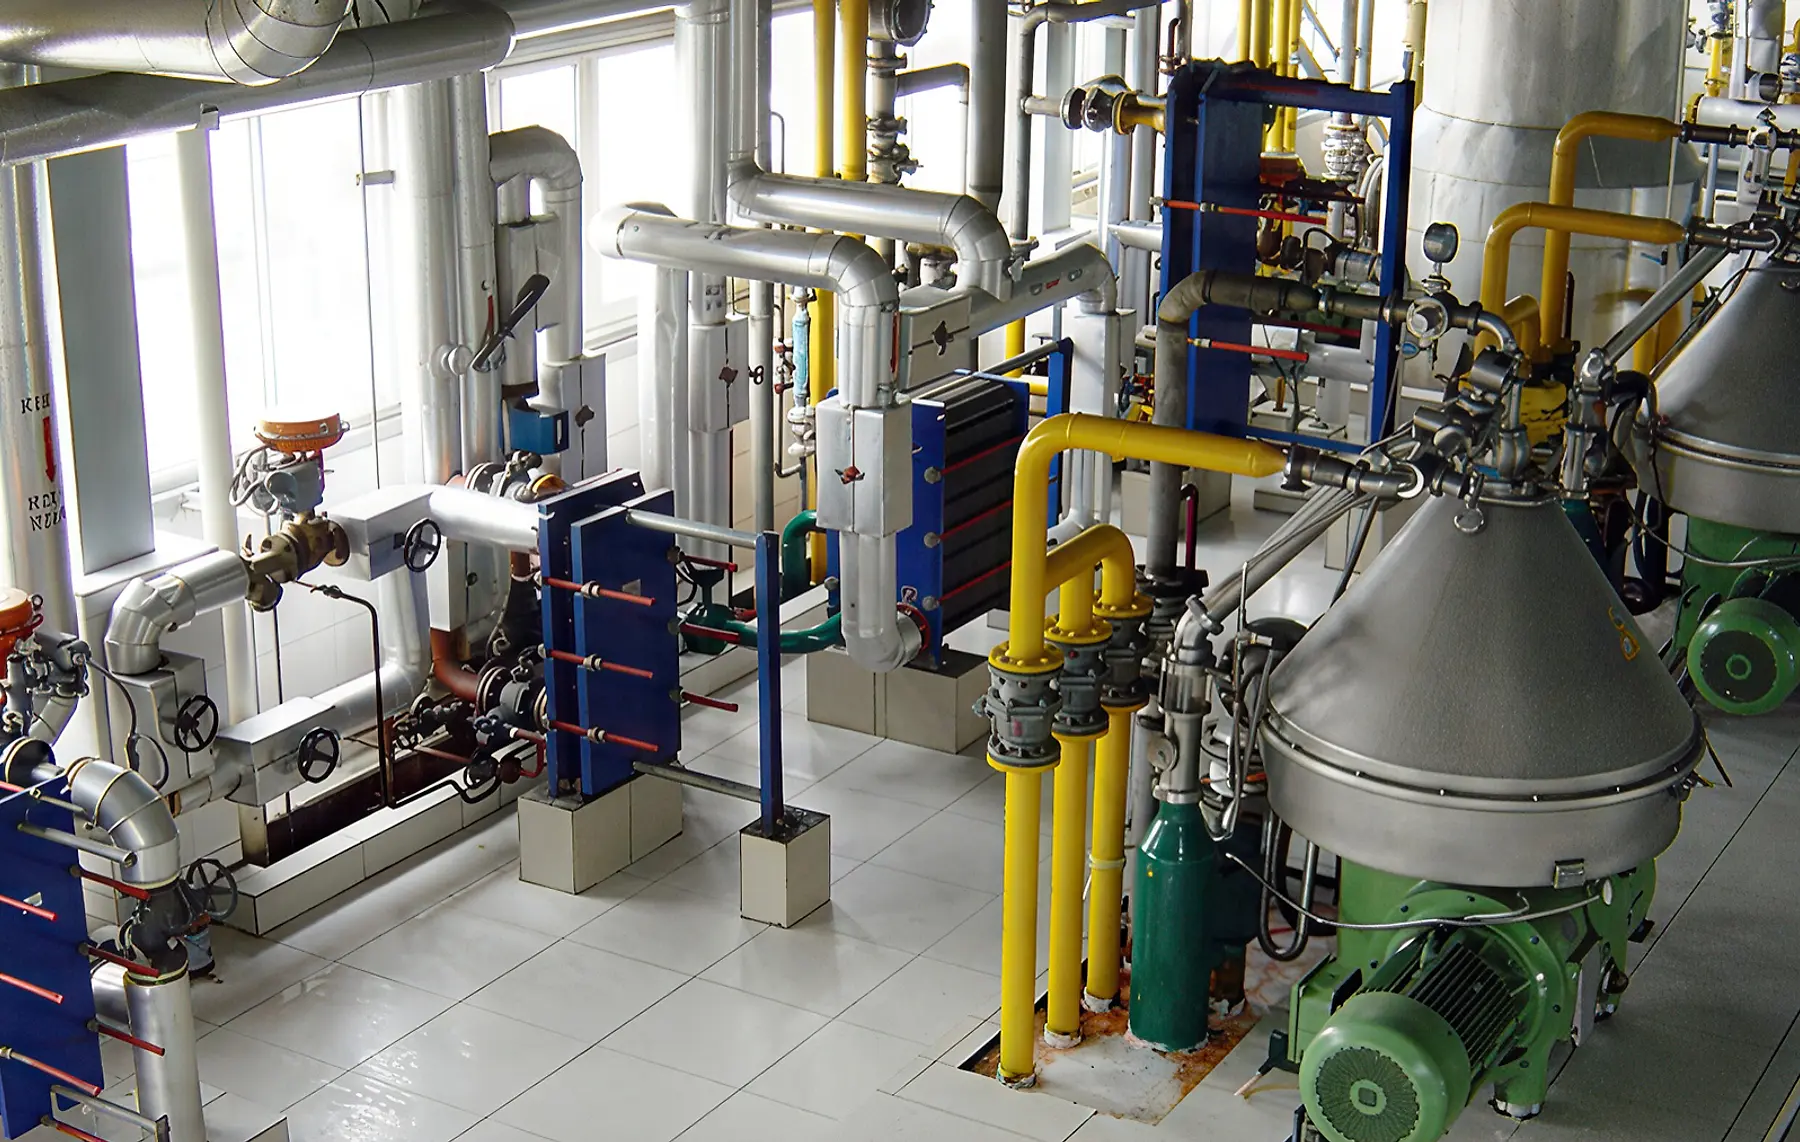 Refinery
The first critical stage in edible oil refining. Removes phospholipids (gums), mucilage, trace metals, and impurities that affect oil quality, color, and stability. Ensures smoother downstream bleaching and deodorizing stages.
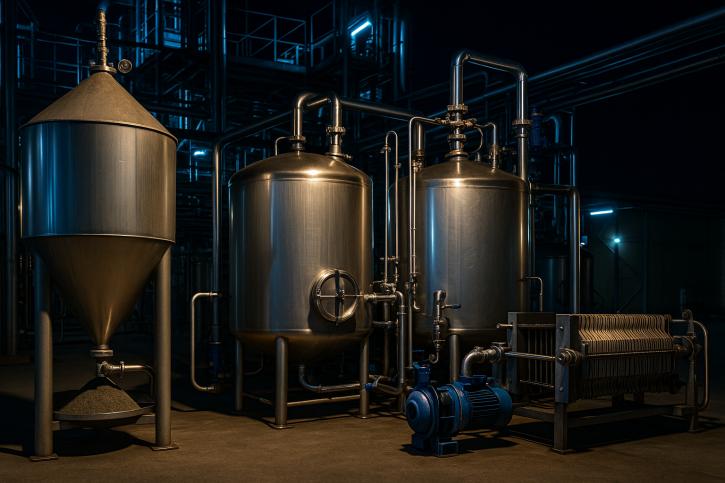 Refinery
Designed to remove color pigments, oxidation by-products, phospholipids, trace metals, and residual impurities under precisely controlled temperature and vacuum conditions. Produces high-quality, light-colored, and stable oil ready for deodorization.
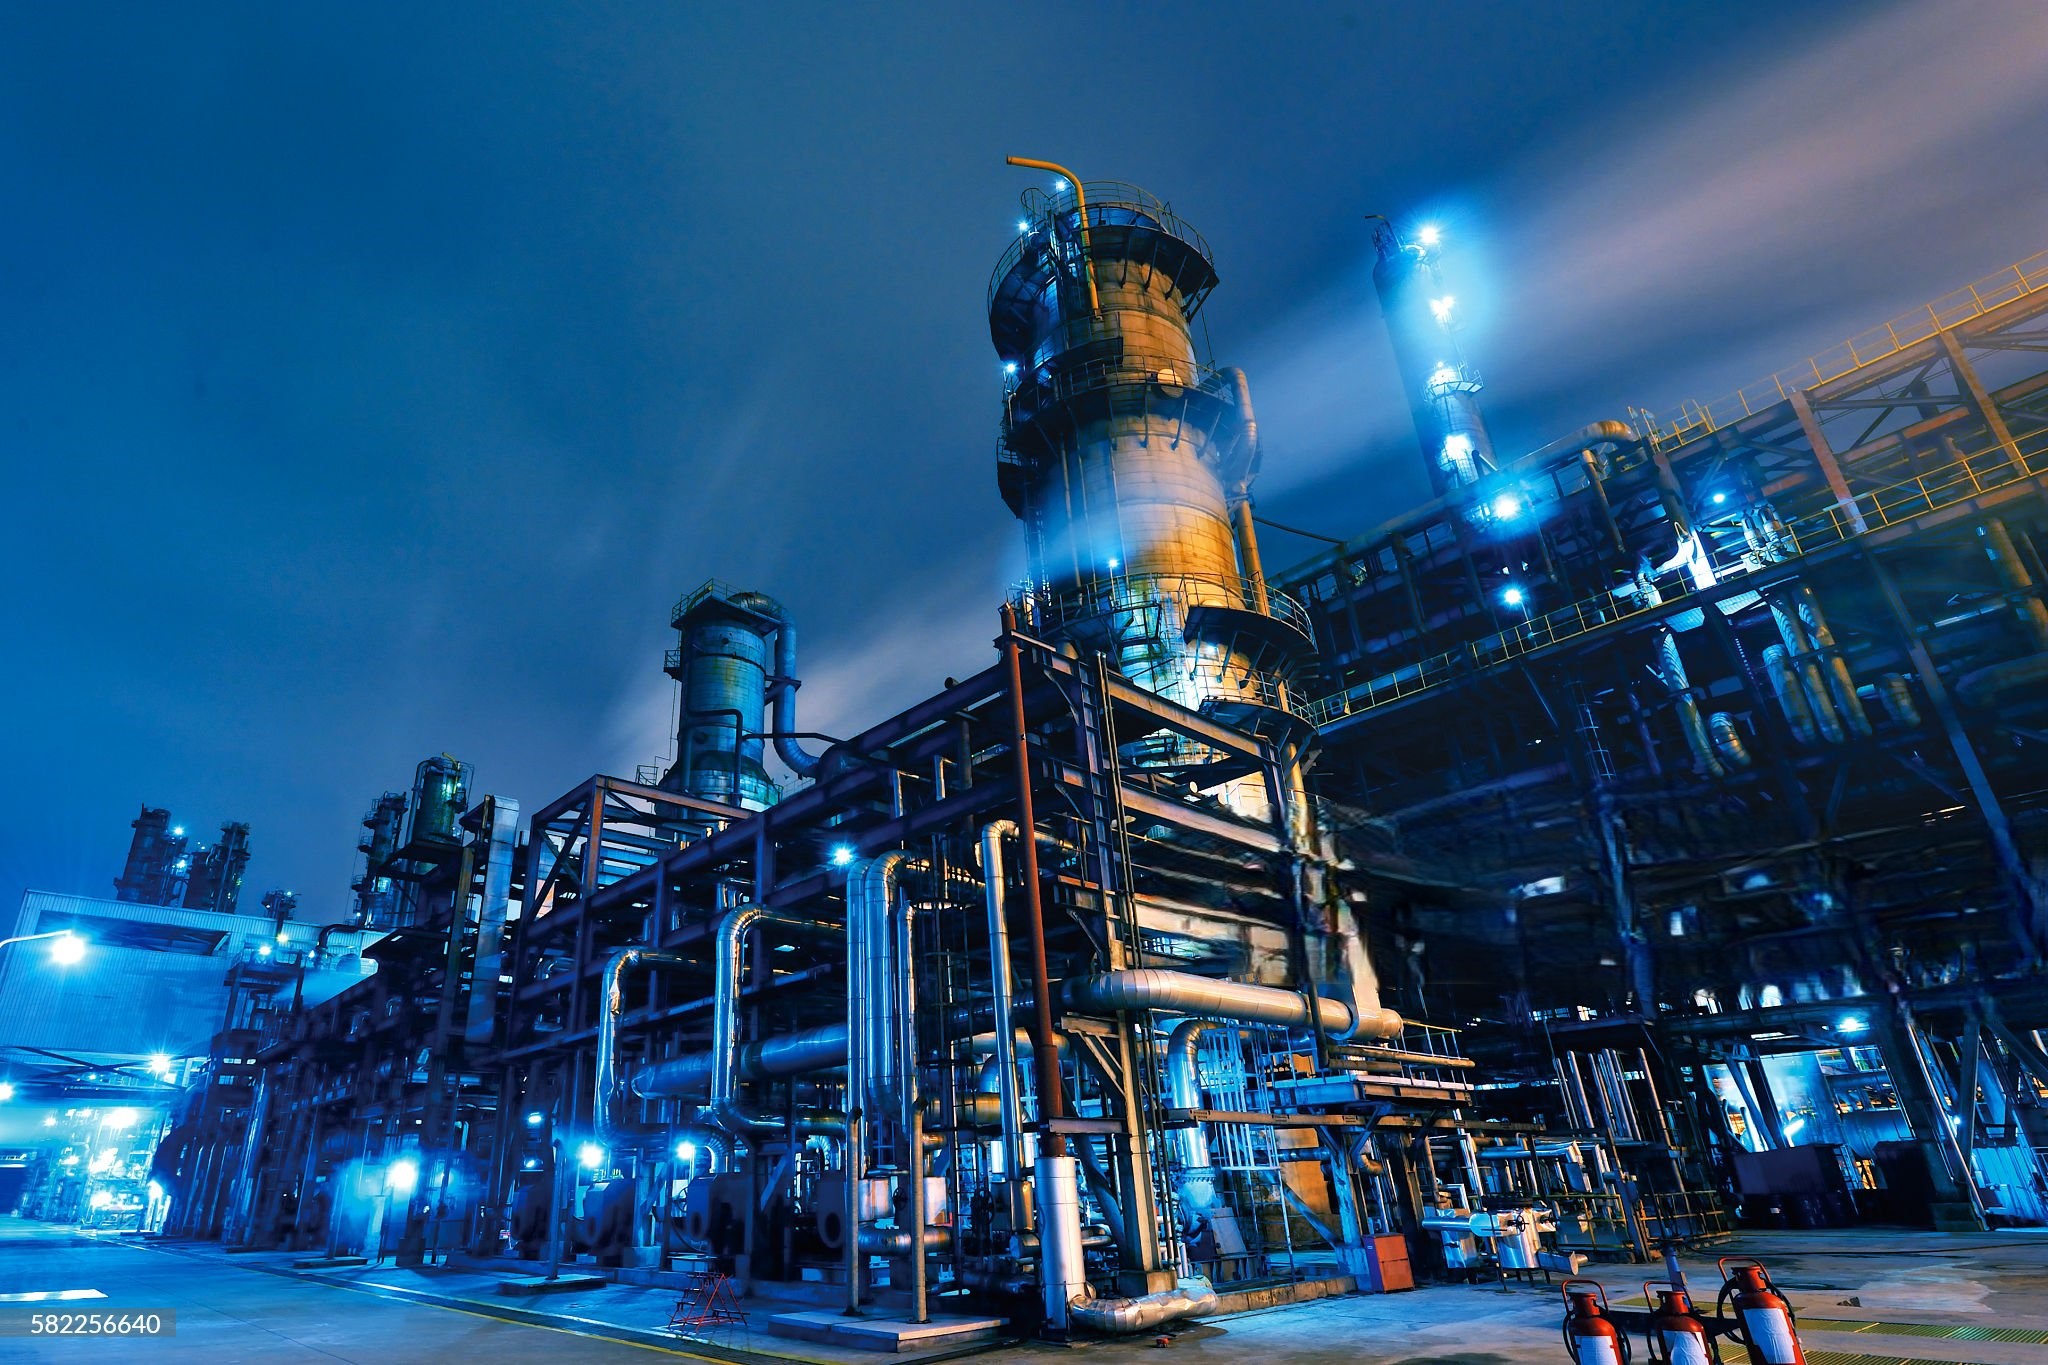 Refinery
High-vacuum, steam-stripping deodorizer column designed to remove ketones, aldehydes, and volatile odor compounds under high temperature. Produces bright, stable, bland edible oil meeting international food-grade standards.
Extraction
Efficiently extracts residual oil from oilseeds and press cake using hexane solvent. The system includes the Extractor, DTDC (Desolventizer-Toaster-Dryer-Cooler), condenser, and solvent recovery units for maximum oil yield and optimal solvent recovery.
Utility
Robust multi-pass thermal exchange system engineered to utilize outgoing hot refined oil to pre-heat incoming crude feed. Drastically reduces fuel consumption and improves plant-wide energy efficiency through integrated heat recovery loops.
Specialty
Produces premium-grade, food-safe lecithin by removing gums, impurities, and moisture through controlled processing. Includes Lecithin Dryer, Settling Tank, Degumming Reactor, and Filtration Unit — ideal for pharmaceutical, food, and feed industries.
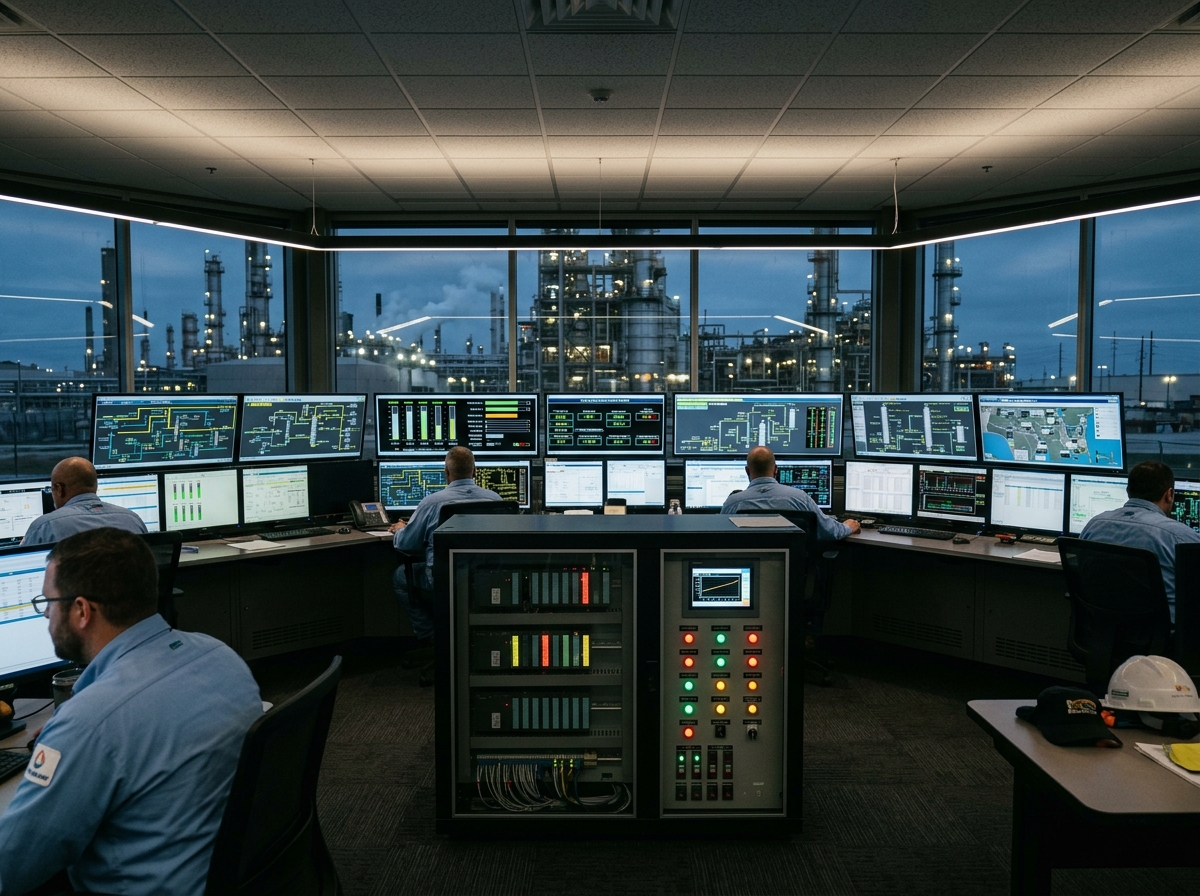 Auxiliary
The centralized automation nerve centre hosting PLC indicators, logic controllers, VFD drives, safety interlock relays, and real-time flow regulators. Supports fully automated or semi-automated refinery operations for reduced manpower and enhanced safety.
| Category | Systems / Equipments | Primary Purpose |
|---|---|---|
| Refinery Section | Neutralizer, Bleacher, Deodorizer, Dewaxing Unit | Removes impurities, phospholipids, coloring pigments, waxes, and free fatty acids (FFA). |
| Solvent Extraction | Extractor, DTDC (Desolventizer-Toaster), Condenser | Recovers remaining vegetable oil content from pressed seeds and oil cakes. |
| Boiler & Utility | Steam Boiler, Heat Exchangers, Storage Vessels | Generates and distributes thermal and mechanical energy to the process loops. |
| Auxiliary Systems | Filters, Pumps, Piping networks, Electrical Panels | Supports automation, chemical dosing, safety interlocks, and fluid conveying. |
| Lecithin Plants | Lecithin Dryer, Settling Tank, Degumming Reactor, Filtration | Produces high-value food grade lecithin by drying separated gums. |
| Biodiesel Plant | Transesterification Reactor, Methanol Recovery Unit, Storage | Converts poor-grade vegetable oils and acid oils into biodiesel and glycerol. |
| S.No | Client Name | Installation Location | Project Executed |
|---|---|---|---|
| 1 | M/s Kaithal Solvent Pvt Limited | Haryana | Refinery Crystallizer System |
| 2 | M/s Vaibhav Edible Oil Pvt Ltd | Kanpur, UP | 600 TPD Continuous Oil Refinery |
| 3 | M/s Lahariya Oil Pvt Limited | Rania, Kanpur, UP | 200 TPD Edible Oil Refinery |
| 4 | M/s. Karsini Eco Board Pvt Limited | Sitapur, UP | Complete Particle Board Plant |
| 5 | M/s. Vaishno Enterprises | Rania, UP | Industrial Storage Warehouse |
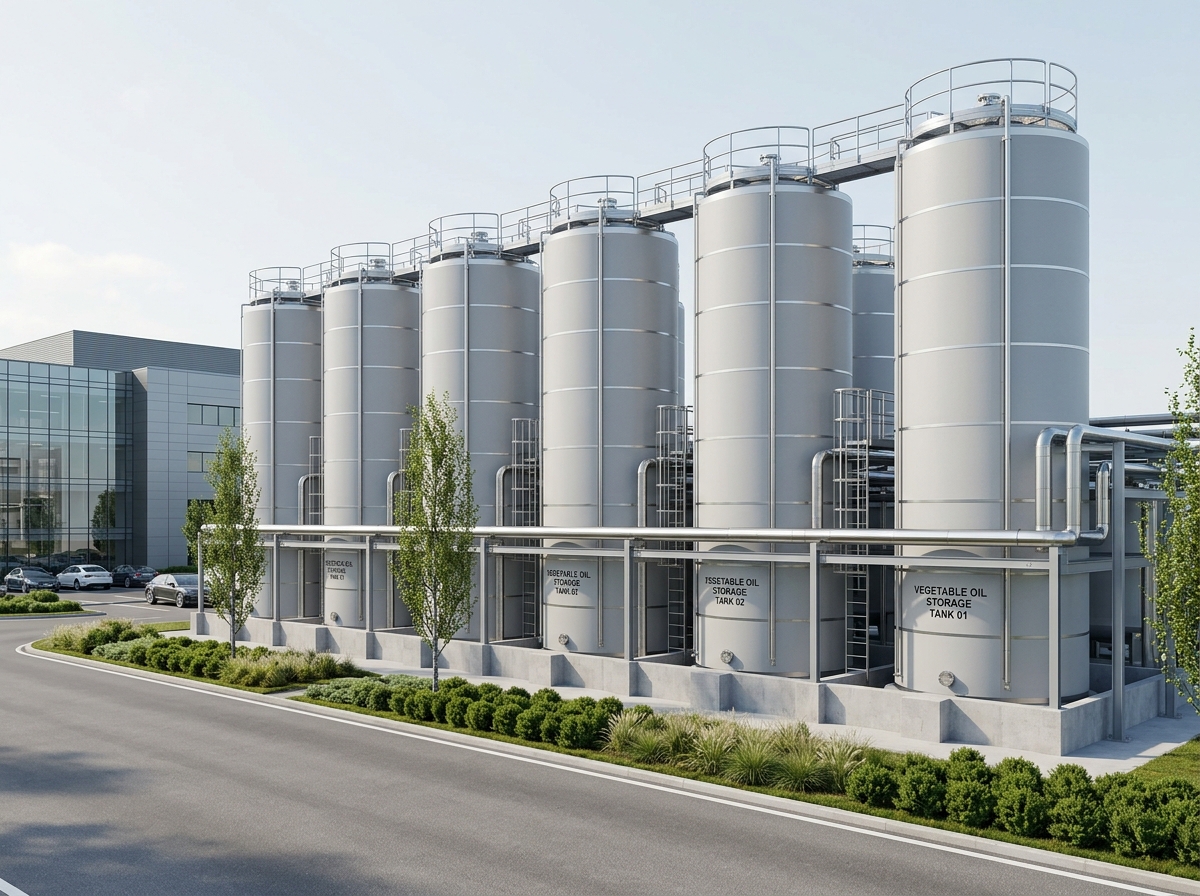
| 6 | M/s. Kanpur Logistic Park | Kanpur Nagar, UP | Industrial Oil Storage Tank Farm |
| 7 | M/s. Rachit Iron Steel Pvt Ltd. | Umran Rania, UP | Heavy Engineering Warehouse structure |
| 8 | M/s. Maruti Nandan Chemical | Kanpur, UP | Bio Desalination Plant |
| 9 | M/s Mantora Oil Pvt Ltd | Kanpur Rania, UP | 200 TPD Refinery Erection |
| 10 | M/s Flavicons Eco Board Pvt Ltd | Unnao, UP | Particle Board Production Line |
| 11 | M/s. Pooja Solvent Pvt Ltd | Banda, MP | Solvent Extraction Plant Installation |
| 12 | M/s. Saray Vala Pvt Ltd. | Krishnapatnam Port, AP | 700 TPD Large-Scale Oil Refinery |
| 13 | M/s. Basant Oil Pvt Ltd. | Mathura, UP | 200 TPD Oil Refinery Plant |
| 14 | Shree Hanumant Enterprise | Lucknow, UP | Heavy Duty Warehouse & Storage Tanks |
| No installations match your search query. Please try searching something else. | |||
Discuss your edible oil refinery setup, custom fabrication requirements, or project estimation query with director Mr. Sanjay Sharma.
M/S. Sanjay Sharma Consultancy of Engineering
988, B-Block, Panki, Kanpur Nagar, UP, India
Charu Techno Projects Unit
1377, Umran Rania, Kanpur Dehat – 209311 (UP), India